Sustainability in Plastic Packaging: How Elham MultiPlast Is Adapting
September 30, 2026
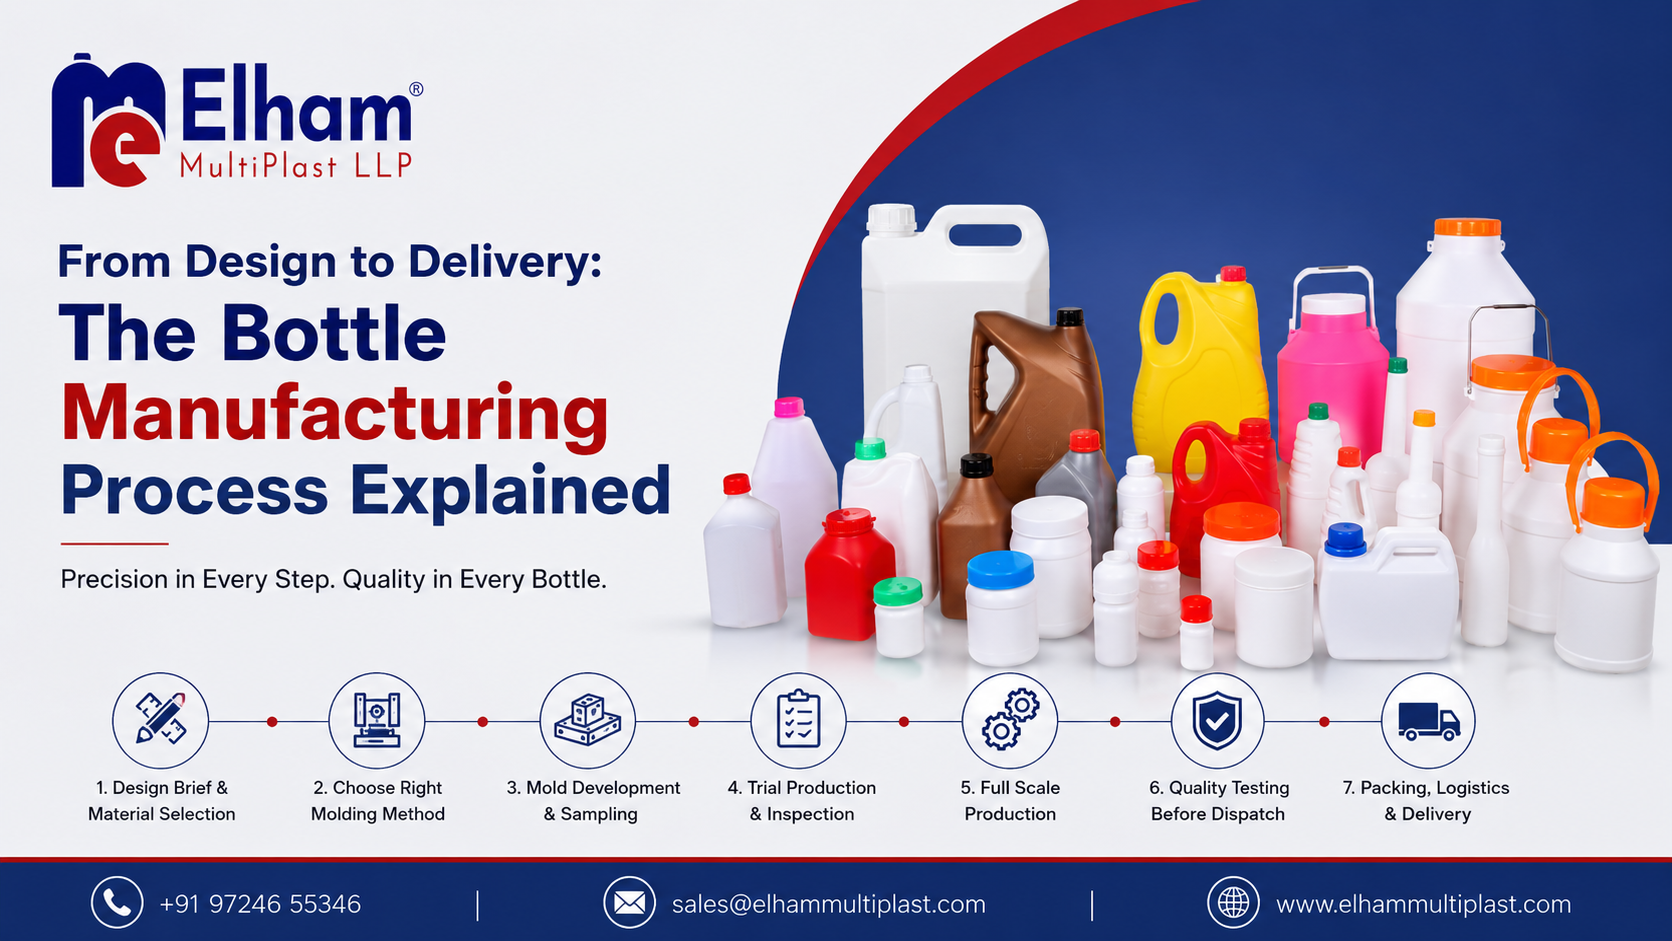
Most first-time packaging buyers only see two moments in the plastic bottle manufacturing process: the design conversation at the start and the finished cartons arriving at the end. Everything in between, mold development, resin selection, trial runs, and quality testing, tends to stay invisible until something goes wrong. Understanding what actually happens at each stage makes it far easier to set realistic timelines, ask the right questions, and avoid the surprises that catch first time buyers off guard.
This guide walks through the full journey a bottle takes from a design brief to a delivered pallet, written for startups, packaging buyers, and product manufacturers who want to understand the process before they commit to an order rather than after.
A typical rigid plastic bottle moves through seven stages between concept and dispatch:
Design brief and material selection
Choosing the right molding method for that material
Mold development and sampling
Trial production and first article inspection
Full scale production
Quality testing before dispatch
Packing, logistics, and delivery
Every project starts with the basics: fill volume, intended product, neck finish, and how the bottle will be filled, capped, and labeled downstream. This is also where custom bottle design decisions around resin get made. A manufacturer worth working with will ask about your product’s chemical makeup before recommending HDPE, PET, or PP, since the wrong resin choice at this stage causes problems no amount of good molding can fix later.
If you already have a rough sketch or a competitor bottle you like the shape of, share it now. It shortens the design conversation considerably compared to starting from a blank page.
Not all blow molding bottles are made the same way, and the method depends heavily on the resin chosen in Stage 1.
Used mainly for HDPE and PP containers. A tube of molten plastic, called a parison, is extruded and clamped inside a mold, then inflated with compressed air until it takes the mold’s shape. This method is well suited to opaque, chemically resistant bottles used for detergents, lubricants, and agrochemicals, and it can produce integral handles in a single step.
Used mainly for PET containers. A preform, a small tube shaped roughly like a test tube with a finished neck, is injection molded first, then reheated and stretched both vertically and radially inside a blow mold. This two-stage approach produces the clarity, precise neck dimensions, and lighter weight typical of PET bottles used for edible oil, personal care, and food contact packaging.
Knowing which method applies to your bottle helps you ask sharper questions about tooling cost, cycle time, and what design features are realistically achievable.
Once the design and molding method are settled, the manufacturer moves into mold development. This typically starts with a 3D design file, followed by mold fabrication, and finally a first sample run used to check that the physical bottle matches the design intent. Complex shapes, custom embossing, or non-standard neck finishes generally take longer to tool than a straightforward stock shaped bottle.
This is the stage where costs and timelines vary the most between suppliers. A transparent manufacturer will explain, in writing, how tooling cost is structured and what happens if the first sample needs adjustment before approval.
Before committing to a full production run, a short trial batch is produced to confirm that the mold performs consistently outside of a single hand built sample. This trial batch is checked for wall thickness consistency, neck and closure fit, and overall dimensional accuracy against the approved design. Any adjustments to machine settings or, in rare cases, the mold itself happen at this point, before large volumes of resin are committed.
With the trial approved, the order moves into full production. This is where bottle production Gujarat facilities with multiple machines and dual manufacturing units have an advantage, since larger or time sensitive orders can be split across lines without pushing everything through a single bottleneck. Machine settings established during the trial phase are held steady throughout the run to keep every bottle in the batch consistent.
A production run is not considered complete once bottles come off the line. Reputable manufacturers run a standard battery of physical tests before any batch is cleared for dispatch:
Torque test, confirming caps tighten securely and hold pressure without loosening in transit
Leakage test, verifying the bottle and closure combination stays fully sealed
Drop test, simulating handling and transport shocks without cracking
Burst strength test, checking resistance to cracking under internal pressure
These are the same checks described on our quality assurance page, and they exist to catch defects before a bottle reaches your filling line rather than after.
The final stage covers how bottles are packed for transit, whether on pallets for domestic dispatch or in Full Container Load shipments for export orders, and how that packing is designed to prevent crushing or shifting in transit. For businesses sourcing across state lines or internationally, ask specifically how the supplier’s HDPE bottles manufacturer operation handles long haul dispatch, since packing standards that work for a local delivery often are not sufficient for a multi day freight journey.
| Stage | What happens | Buyer’s role |
| 1. Design brief | Fill volume, neck finish, and resin are defined | Share references and product chemistry |
| 2. Molding method | Extrusion or injection stretch blow molding is selected | Confirm feasibility of design features |
| 3. Mold and sampling | Mold is fabricated and a first sample is produced | Review and approve or request changes |
| 4. Trial run | Small batch checked for consistency and fit | Sign off before full production begins |
| 5. Full production | Order is produced at volume across production lines | Confirm delivery milestones |
| 6. Quality testing | Torque, leak, drop, and burst tests are run on the batch | Request test reports if needed |
| 7. Packing and delivery | Bottles are packed and dispatched domestically or for export | Confirm freight terms and delivery address |
Timelines vary significantly depending on whether you are ordering an existing stock design or commissioning a new mold. A stock design that only needs color and label changes can often move to production quickly, since mold development is skipped entirely. A new custom mold adds design, fabrication, and sampling time before production can begin, and complex shapes or non-standard neck finishes typically extend that window further. Rather than relying on a single generic number, ask your manufacturer for a written timeline broken down stage by stage, referenced against a past project of similar complexity.
Blow molding is used to make hollow plastic containers, most commonly bottles and jars, by inflating heated plastic inside a mold. It is the standard process behind the majority of HDPE and PET packaging on the market.
Extrusion blow molding shapes a plastic tube directly inside a mold and is typically used for HDPE and PP containers. Injection stretch blow molding first creates a small preform, then reheats and stretches it into the final bottle shape, and is the standard method for PET containers that need clarity and precise neck dimensions.
It depends on design complexity, but simple shapes generally move faster than bottles with custom embossing, handles, or non-standard neck finishes. Ask your supplier for a written estimate tied to your specific design rather than a generic industry average.
Yes, and it is usually higher for a new mold than for an existing stock design, since the mold cost needs to be offset across the order volume. Some manufacturers offer staggered production or shared tooling arrangements to reduce the initial commitment.
Reliable manufacturers run torque, leakage, drop, and burst strength tests on production batches before dispatch. Ask to see sample test reports if quality documentation matters for your own compliance or brand standards.
Knowing what happens between a design brief and a delivered pallet turns a plastic bottle order from a black box into a process you can actually manage. At Elham MultiPlast LLP, this journey runs across two production units in Himmatnagar and Surat, Gujarat, covering HDPE, PET, and PP bottles and jars for detergent, agrochemical, edible oil, lubricant, veterinary, and personal care applications.
If you are planning a new bottle design or need a PET bottles manufacturer for an existing product line, our team can walk you through resin selection, mold timelines, and sampling before you commit to a full order. Reach out through our contact page to start that conversation, or browse our plastic bottle manufacturer in Sabarkantha facilities and capabilities in more detail.
Sustainability in Plastic Packaging: How Elham MultiPlast Is Adapting
September 30, 2026
From Design to Delivery: The Bottle Manufacturing Process Explained
September 30, 2026
Top 5 Factors to Consider When Choosing a Plastic Bottle Manufacturer in India
September 30, 2026
Edible Oil Packaging: Why HDPE Cans Are the Preferred Choice
September 28, 2026
How Agro Chemical & Pesticide Bottles Are Manufactured for Safety and Compliance
September 28, 2026
Veterinary Bottle Packaging: Ensuring Safety for Animal Health Products
September 28, 2026